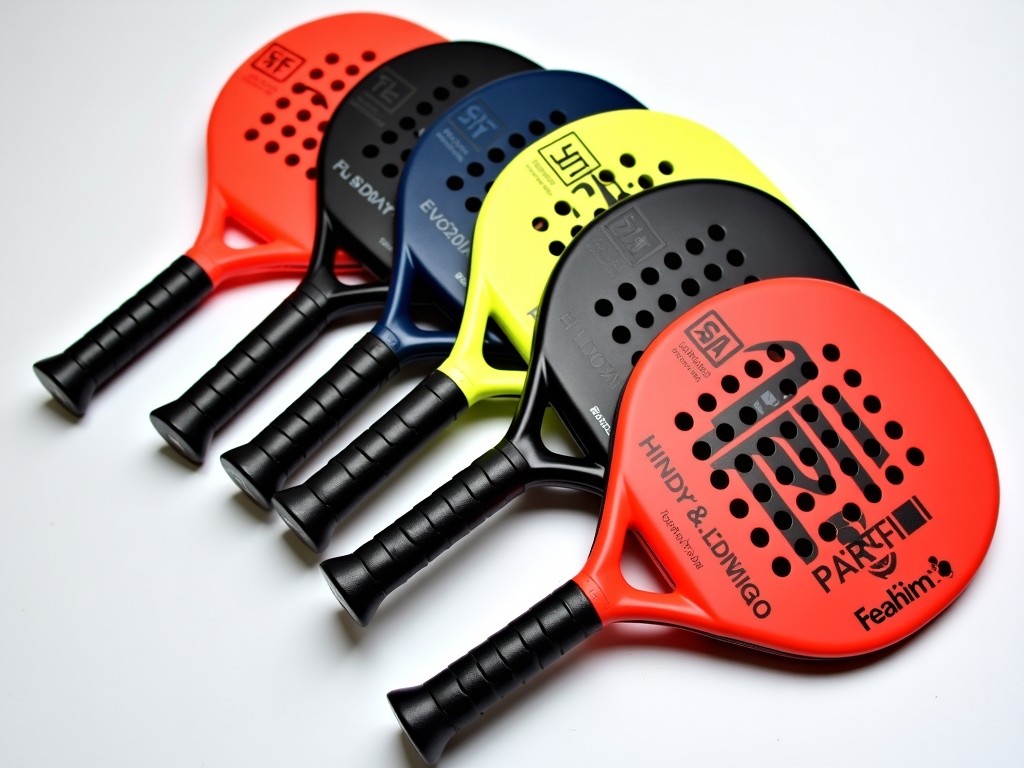
Factory Direct Ianoni Padel Racket Supplier
Ianoni manufactures padel rackets in a dedicated facility that controls raw material intake, lay‑up processes, and final finishing. By handling production in‑house, the supplier can adjust lay‑up
Factory Direct Ianoni Padel Racket Supplier
Ianoni manufactures padel rackets in a dedicated facility that controls raw material intake, lay‑up processes, and final finishing. By handling production in‑house, the supplier can adjust lay‑up schedules, monitor resin cure cycles, and ship directly to distributors without intermediary handling. This approach reduces lead‑time variability and provides traceability from fiber lot to finished racket.
Technical Specifications
| Parameter | Typical Range | Measurement Method |
|---|---|---|
| Length | 455 mm ± 2 mm | Caliper measurement from butt to tip |
| Width (max) | 260 mm ± 2 mm | Caliper across frame |
| Weight (unstrung) | 340 g ± 5 g | Precision scale (±0.1 g) |
| Balance Point | 260 mm ± 3 mm from butt | Balancing beam |
| Swing Weight | 260 kg·cm² ± 10 kg·cm² | Pendulum method |
| Stiffness (RA) | 68 ± 3 | RA meter (flexural) |
| String Pattern | 16 main × 19 cross | Visual count |
| Grip Size | 4 ¼ in (L0) – 4 ⅝ in (L3) | Caliper on grip |
Materials and Construction
The racket frame uses a unidirectional carbon fiber prepreg with a fiber volume fraction of approximately 58 %. The core is a high‑density EVA foam (density 0.22 g/cm³) injected into a molded cavity, providing a consistent stiffness gradient. A surface layer of 3K woven carbon fiber adds abrasion resistance and contributes to the final RA value. All plies are oriented according to finite‑element analysis that targets a first‑mode bending frequency around 115 Hz.
- Carbon fiber: T700SC, 12 k tow, epoxy resin system
- EVA core: closed‑cell, shore hardness 45 A
- Surface finish: matte UV‑cured coating, 15 µm thickness
Manufacturing Process
Lay‑up begins with laser‑cut prepreg plies placed on a temperature‑controlled mold. Vacuum bagging applies 0.8 bar pressure while the mold is heated to 130 °C for a 90‑minute cure cycle. After demolding, the foam core is injected under vacuum to ensure full cavity fill and avoid voids. The racket then undergoes a post‑cure at 160 °C for 30 minutes to stabilize the resin system. Final machining defines the throat geometry and installs the butt cap and grommets.
Quality Control
Each racket is weighed and balanced before stringing. A random sample of 5 % per batch undergoes ultrasonic C‑scan to detect delamination or resin‑rich zones. Flexural stiffness is measured on a three‑point bend fixture; parts deviating more than ±3 % from the target RA are re‑evaluated. String tension loss is monitored after 24 hours at 22 °C/50 % RH to verify frame integrity. All data are logged against the material lot number for traceability.
Applications
Padel rackets from Ianoni are suited for clubs that require a consistent feel across multiple courts, as the tight weight tolerance (±5 g) minimizes player‑to‑player variation. The balanced swing weight (~260 kg·cm²) supports both control‑oriented baseline play and aggressive net approaches, making the design versatile for intermediate to advanced players. The high‑density EVA core reduces vibration transmission, which helps decrease arm fatigue during prolonged match play.
Customization Options
- Weight adjustment: ±10 g via internal tungsten inserts
- Balance shift: head‑light or head‑heavy configurations (±15 mm)
- Grip size: L0 to L4 with optional over‑wrap thickness
- String pattern: 14 × 18, 16 × 19, or 18 × 20 on request
- Cosmetic: matte, gloss, or custom color graphics (Pantone matched)
Packaging and Logistics
Rackets are placed in individual corrugated sleeves with internal foam end caps, then packed five per master carton (dimensions 380 mm × 260 mm × 120 mm). Each carton receives a poly‑strapping band and a humidity indicator card. Palletized shipments use 1.2 m × 1.0 m × 1.6 m pallets with stretch film and corner boards to withstand forklift handling. Export documentation includes a material safety data sheet for the epoxy system and a certificate of origin upon request.
FAQ
- Can dimensions be customized?
Yes, length, width, and throat geometry can be adjusted within ±5 mm limits based on mold tooling availability. - What information is required before quotation?
Required details include target weight range, preferred balance point, grip size, string pattern, and any cosmetic or branding specifications. - What materials are available?
Standard carbon fiber/T700SC prepreg with EVA core; alternative cores (polyethylene foam, hybrid) and fiber grades (T800, M40J) are offered upon request. - How is quality inspected?
Each lot undergoes weight, balance, ultrasonic C‑scan (5 % sample), and flexural stiffness testing; results are retained for traceability. - What packaging methods are available?
Standard single‑sleeve + master carton; options include double‑wall cartons, reusable plastic cases, or pallet‑less bulk packing. - How are export shipments protected?
Cartons are strapped, humidity‑checked, and placed on film‑wrapped pallets with corner boards; additional insurance can be arranged. - What is the typical production lead time?
Lead time ranges from 3‑4 weeks for standard configurations to 6‑8 weeks for fully customized orders, depending on tooling and material availability. - How are samples arranged?
Sample rackets (up to two units) can be shipped via express courier after approval of a sample request form; costs are credited against the first production order.
Contact Ianoni for a Quote
To discuss technical requirements, request a sample, or receive a detailed quotation, please reach out to our engineering team. Provide your performance targets, quantities, and any special considerations so we can prepare an accurate response.
Request a Quote →


